ByJohn A
When Positioning Accuracy Traces Back to the Guide Rods, Not the Controller
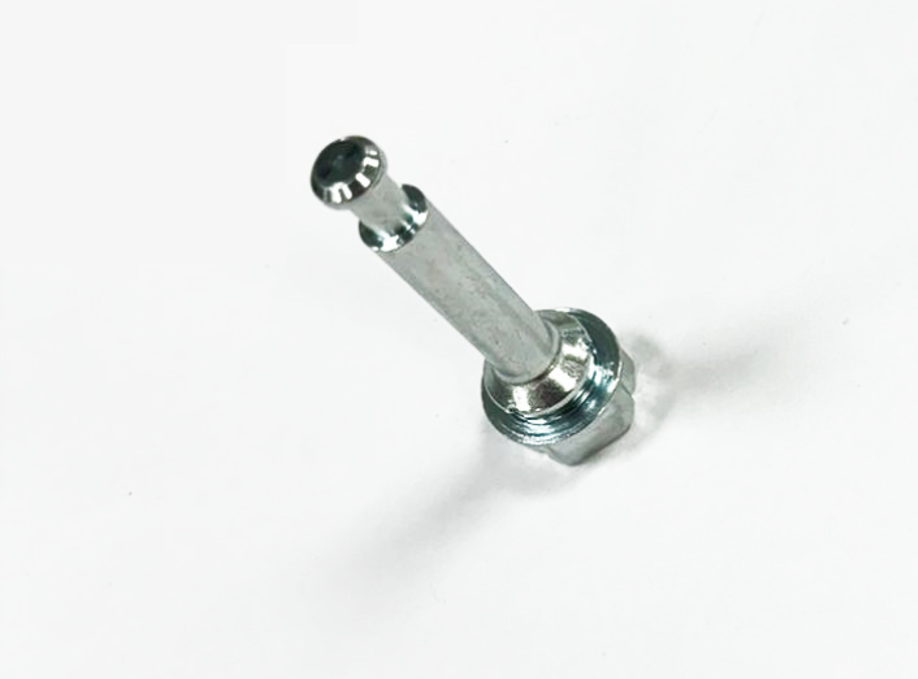
A machine starts missing its position by a few microns, and the first suspect is almost always the control system. Someone pulls up the servo tuning. Someone else checks the encoder count. Hours go by, the parameters get adjusted twice, and the same reading is still showing on Monday morning. The part that rarely gets checked first sits in plain view on the machine bed. Guide rods carry the moving assembly, and when they lose their form, every command the controller sends arrives slightly off target.
Here is the awkward part. The controller reports success. It moved the axis exactly as instructed, and the encoder agrees. What the encoder cannot see is the carriage drifting sideways on worn guide rods while the count says everything is fine. That gap between the reported position and the real position is where scrap comes from, and it quietly grows over months.
Why the Controller Reports a Move It Did Not Actually Make
Most feedback loops measure rotation at the motor or track travel along a single line. They do not measure whether the carriage stayed square.
Picture a rod with a slight bow in the middle. The bearing rides through that section, lifts a fraction, then settles again at the far end. The motor position is correct but the tool position is not. Nothing in the loop flags it.
This may be why the reading looks so unusual when it first appears. It shows up at one point in the stroke and clears elsewhere. Tuning works on the control loop, while a geometry issue calls for a mechanical fix, which is where a week can go before the cause is identified.
Reading the Symptom Pattern Before Touching the Servo Loop
Some patterns point away from control and toward the guides. Watch for these.
- Reading changes with position in the stroke, not with speed or load.
- Repeatability is consistent in one direction and looser in the other.
- The fault worsens through a shift as the machine warms.
- The surface finish on the part changes before the dimensional deviation appears.
- Two identical machines drift differently, though they run the same program.
That last one matters more than it looks. Software is identical across both machines. Hardware wear is not.
What Wear on Guide Rods Actually Does to Accuracy
The rod surface is the running track for the bearing. Nothing sits between them. So the hardness and finish of that surface decide how long the fit lasts.
Recirculating balls press into a soft or rough track, opening the clearance. Once clearance opens, the carriage has room to move without the motor turning. That free movement is a source of positional deviation, and software compensation works on repeatable effects rather than on movement of this kind.
The National Institute of Standards and Technology has published extensively on machine tool accuracy budgets, and geometric deviation from guideways consistently ranks among the larger contributors in precision positioning work. Straightness deviation feeds directly into the axis’s volumetric accuracy.
Wear also feeds itself. Play lets the bearing cock slightly under load, which loads the balls unevenly, which wears the track faster. A slow problem becomes a fast one.
Straightness Tolerance and the Slow Loss of Repeatability
New rods leave the grinder within a tight straightness limit. That limit is not permanent.
Mounting stress bends them. An over-torqued support block, a base that is not flat, a machine dropped hard on a shipping pallet. Any of these puts a bow into a rod that is measured perfectly on the inspection bench.
Then there is the case depth question. A hardened case over a ductile core works well until the case is worn through in the heavily used section of the stroke. After that, the wear rate climbs steeply, because the softer core underneath was never meant to carry a bearing.
Let’s break it down into checks you can run this week.
- Sweep a dial indicator along each rod against a straightedge, at several rotations.
- Measure diameter at both ends and at mid-stroke, looking for a worn band
- Feel for play by pushing the carriage laterally with the drive disengaged.
- Check the support blocks for flatness and confirm mounting torque.
- Look at the track surface under light for dulling, scoring or fine pitting.
See also: Buy Gmail PVA Accounts: A Practical Guide to Choosing Reliable Email Accounts
Specifying Guide Rods That Hold Position Over a Service Life
Replacing worn rods with the same specification restarts the same clock. Buying on diameter alone repeats the original mistake, which is more common than most engineers would admit.
The support style deserves a second look too. An end-supported rod deflects across a long span under load, and that deflection binds the bearing. Fully supported rail mounting removes that problem, at the cost of a heavier assembly.
The next steps are straightforward. Before the next tuning session, measure the guides. Record the numbers against the original specification. If the rods have moved outside their limits, no controller setting will bring the axis back, and every hour spent in the software is an hour the scrap rate keeps running.
Send a drawing showing diameter, hardness, straightness tolerance, finish, and end form to have replacement rods matched to the axis they serve.